Food Packaging Machine Types and the Film or Pouch Inputs They Require
Huasheng Packaging Technical Content Review · Published: · Updated:
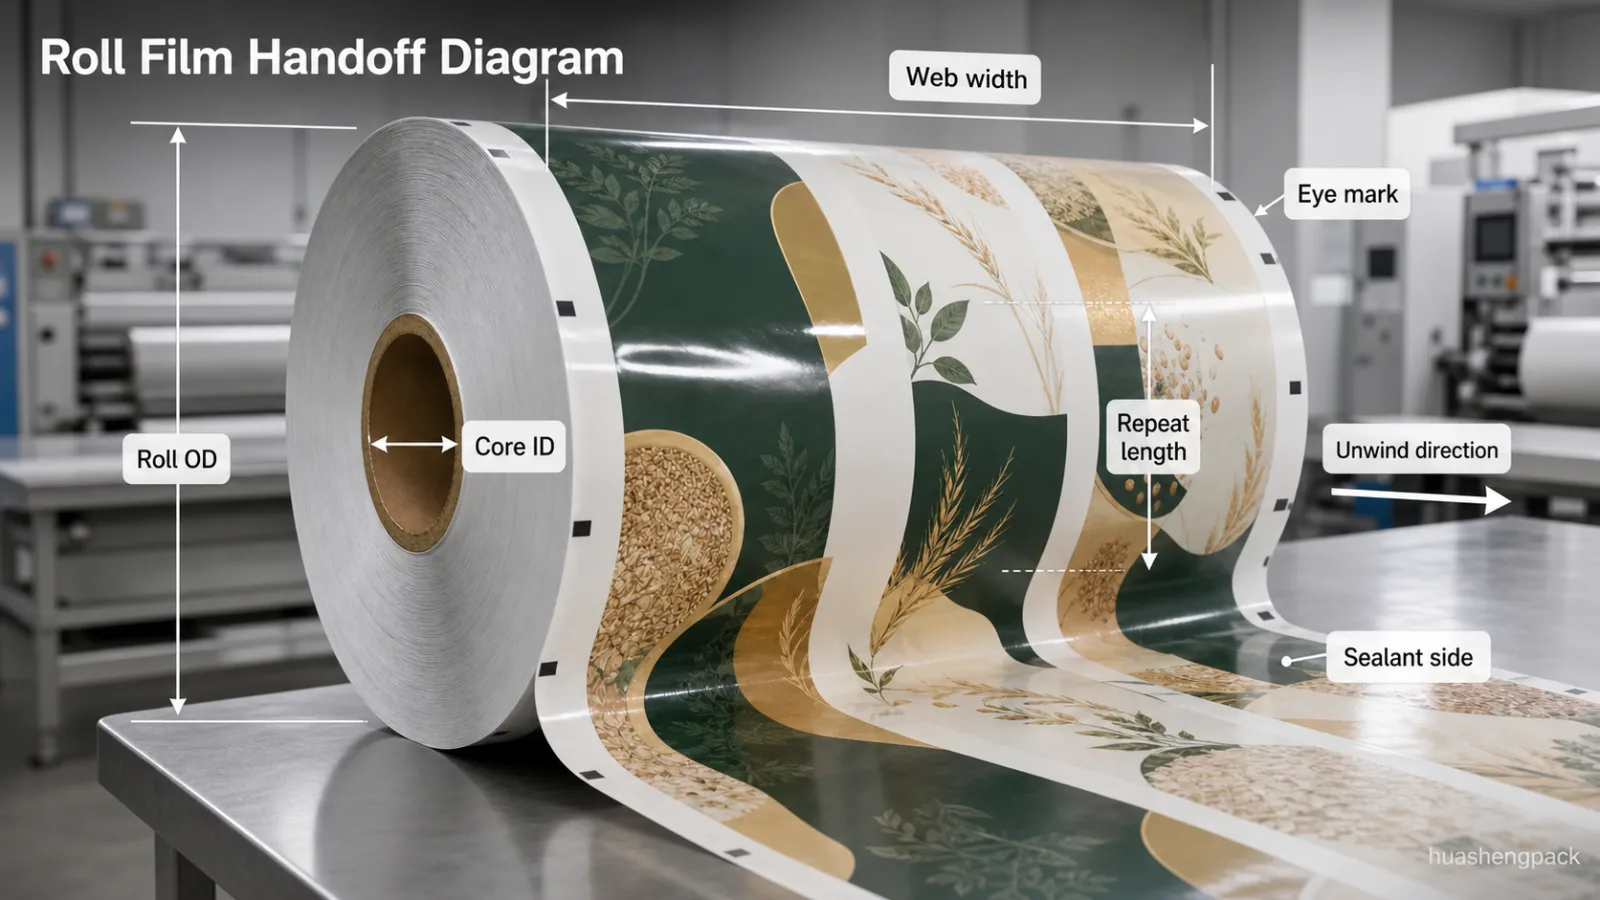 VFFS, HFFS, flow-wrap, premade-pouch and filling lines require different web, pouch, registration, unwind and sealing inputs.
 Name the machine type, make, model and finished pack style before selecting packaging.
Direct answer
VFFS, HFFS, flow-wrap, premade-pouch and filling lines require different web, pouch, registration, unwind and sealing inputs. Name the machine type, make, model and finished pack style before selecting packaging.
Evidence-reviewed technical guide
2026-08-12 · Huasheng Packaging Technical Content Review
Evidence scope
The input differences among VFFS, horizontal flow wrapping and premade-pouch equipment.
Scope and limitations
Manufacturer examples establish architecture and requested inputs only; they do not set industry-wide dimensions, speeds, COF or sealing conditions.
Key takeaways
- Machine category alone is not a specification.
- Rollstock and premade pouches require different handoff data.
- Laboratory COF and heat-seal data do not establish line approval.
Define the operating need
VFFS, HFFS, flow-wrap, premade-pouch and filling lines require different web, pouch, registration, unwind and sealing inputs.
Name the machine type, make, model and finished pack style before selecting packaging.
Machine category is only the start of a packaging brief. A VFFS project must connect the product, dose, bag width and length, forming hardware, web width and repeat, eye-mark and cut relationship, unwind direction, print side, reel limits, sealing arrangement and required operating range. HFFS adds the product infeed and longitudinal-versus-end-seal geometry. A premade-pouch line needs the actual pouch pickup, opening, filling and top-sealing sequence plus closure and fitment details.
Common specification gaps
Width alone is insufficient; repeat, unwind, eye mark, core, reel limits and sealant face also control fit.
Do not approve a film because its nominal width fits the machine. Tracking, forming, stiffness, surface friction, curl, repeat, splice position and seal behaviour can still prevent stable operation. Do not publish one coefficient of friction, core, reel diameter or sealing temperature as an industry value. ISO 8295 measures specified film surfaces under a defined method, while laboratory heat-seal screening is only a starting relationship; neither result alone proves that a particular line will run the package.
Build the decision boundary
Premade-pouch lines need pouch opening, pickup, zipper and dimensional consistency information.
Use a machine-specific handoff sheet and attach the equipment manual, current acceptable reel or pouch, forming-set drawing and photographs of unwind, eye-mark and seal geometry. Identify the product feed, target speed range, start-stop pattern, coding, gas flush or accessories, rejection points and case-packing orientation. Keep supplier alternatives in separate rows. If the machine model or forming set is unknown, mark the project for a line survey or representative trial instead of guessing from a bag photograph.
Validate with evidence
Match film stiffness, friction, sealing window and format to the actual web path and operating range.
Run a representative machine trial and record tracking, registration, forming, filling and sealing.
Approve the first reel or pouch batch through observable stages: startup, registration and tracking, forming or opening, filling, longitudinal and transverse sealing, cutting, steady-state running, stop and restart, and finished-pack handling. Record settings as trial observations for that line, not universal material recommendations. Retain the approved reel orientation, splice rule, sample packs and defect map. Laboratory data should be traceable to the same candidate construction and surface tested. Note the trial duration, usable output and reason for every stop without turning them into an industry performance claim.
Information to prepare
Send machine manuals or drawings, sample packs, speed range, jaw layout and current material data.
For quotation, provide the exact machine maker and model, forming hardware, packaging mode, product and feed behaviour, dose, target pack geometry, current material if available, web or pouch dimensions, repeat, eye mark, unwind drawing, print side, core and maximum reel constraints, target running range and seal type. Add coding, zipper, valve, spout, perforation or gas-flush requirements. The deliverable should be a controlled trial plan and input register, not an unsupported promise of machine compatibility. Assign the machine owner, packaging supplier and filler responsibility for every trial observation and unresolved adjustment.
Before production release, record the approved sample, specification revision, evidence reviewed, unresolved exceptions, decision owner and the exact change conditions that require a new review.
Related Products
Related Packaging Guides
Claim-to-source evidence matrix
| Reviewed claim | Support | Sources | Boundary |
|---|
| A VFFS application brief connects product, bag, film, reel, sealing and output inputs. | direct | [1] | No questionnaire value is generalized to another machine. |
| Horizontal flow wrapping forms and seals a package from roll material around horizontally fed product. | direct | [2] | Configuration and operating range remain machine-specific. |
| Premade-pouch equipment handles pouch transfer, opening, filling and sealing as separate operations. | direct | [3] | One OEM model does not define all pouch-machine limits. |
| COF and laboratory heat-seal methods support material screening but do not approve a target line. | direct | [4], [5] | Exact surfaces, forming path, speed and sealing geometry require a representative trial. |
JSON · CSV
Authoritative References
- ROVEMA: VFFS Application Questionnaire · ROVEMA North America · manufacturer-data
A VFFS application brief connects product, bag, film, reel, sealing and required-output inputs - Syntegon: Horizontal Flow Wrapping · Syntegon · manufacturer-data
Horizontal flow wrapping forms and seals a package from roll material around horizontally fed product - Mespack H180SC Premade Pouch Machine · Mespack · manufacturer-data
Premade-pouch equipment handles pouch transfer, opening, filling and sealing as distinct operations - ISO 8295:1995: Plastics — Film and Sheeting — Determination of the Coefficients of Friction · International Organization for Standardization · standard
Coefficient of friction is measured for specified film surfaces under a defined method - ASTM F2029-16(2021): Laboratory Heat Seals for Flexible Barrier Materials · ASTM International · standard
Laboratory heat-seal relationships are starting data and do not replace production-equipment validation
Frequently Asked Questions
What should be confirmed first?
Name the machine type, make, model and finished pack style before selecting packaging.
Which detail is often missed?
Width alone is insufficient; repeat, unwind, eye mark, core, reel limits and sealant face also control fit.
Can one option suit every product?
Premade-pouch lines need pouch opening, pickup, zipper and dimensional consistency information.
What should a trial verify?
Match film stiffness, friction, sealing window and format to the actual web path and operating range.
When should the specification be reviewed?
Run a representative machine trial and record tracking, registration, forming, filling and sealing.
What should be sent to the supplier?
Send machine manuals or drawings, sample packs, speed range, jaw layout and current material data.